Ceramic ultrafiltration (CUF) is a robust solid-liquid separation technology designed for demanding industrial applications. In starch sugar and biochemical processes, hydrolysates and fermentation broths may contain proteins, residual starch, cell debris, and other suspended impurities that need to be removed before downstream purification and concentration.
Our turnkey ceramic ultrafiltration solutions provide filter-aid-free clarification with high chemical and thermal resistance, reliable filtration performance, and long membrane service life.
Membrane Principles & Cross-Flow Filtration
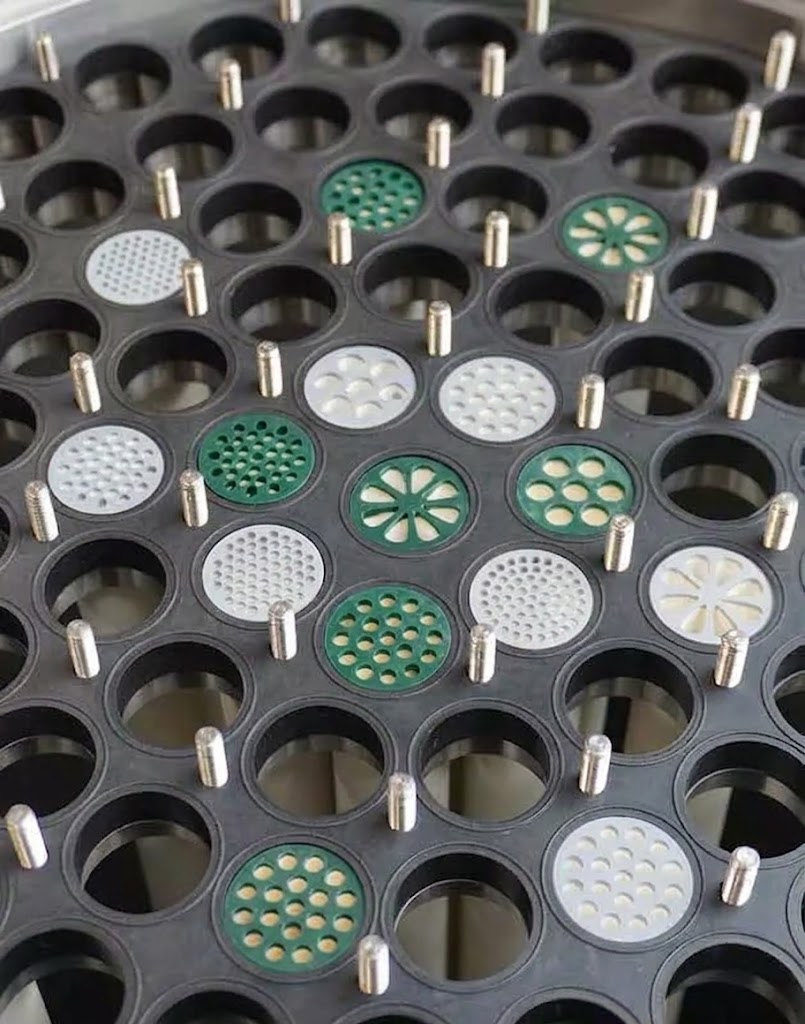
Ceramic membrane systems operate in tangential cross-flow mode using tubular or multichannel membrane elements manufactured from inorganic ceramic materials such as alumina, zirconia, and titania.
Turnkey Process Stages
-
Feed Conditioning & Pre-Screening
Coarse filtration and feed conditioning to remove larger particles and protect membrane channels while maintaining suitable operating conditions.
-
Cross-Flow Membrane Filtration
Recirculation-based ceramic membrane systems designed for stable cross-flow operation, efficient solids separation, and controlled permeate production.
-
Concentration & Diafiltration
Integrated concentration and optional diafiltration stages for improved product recovery and efficient separation of dissolved components from suspended solids.
-
Retentate Management
Controlled collection and handling of concentrated retentate streams, with options for byproduct recovery or further processing.
-
Automated CIP & Cleaning Systems
Automated chemical cleaning and rinsing sequences designed to maintain membrane performance and extend membrane service life.
Engineering & Automation
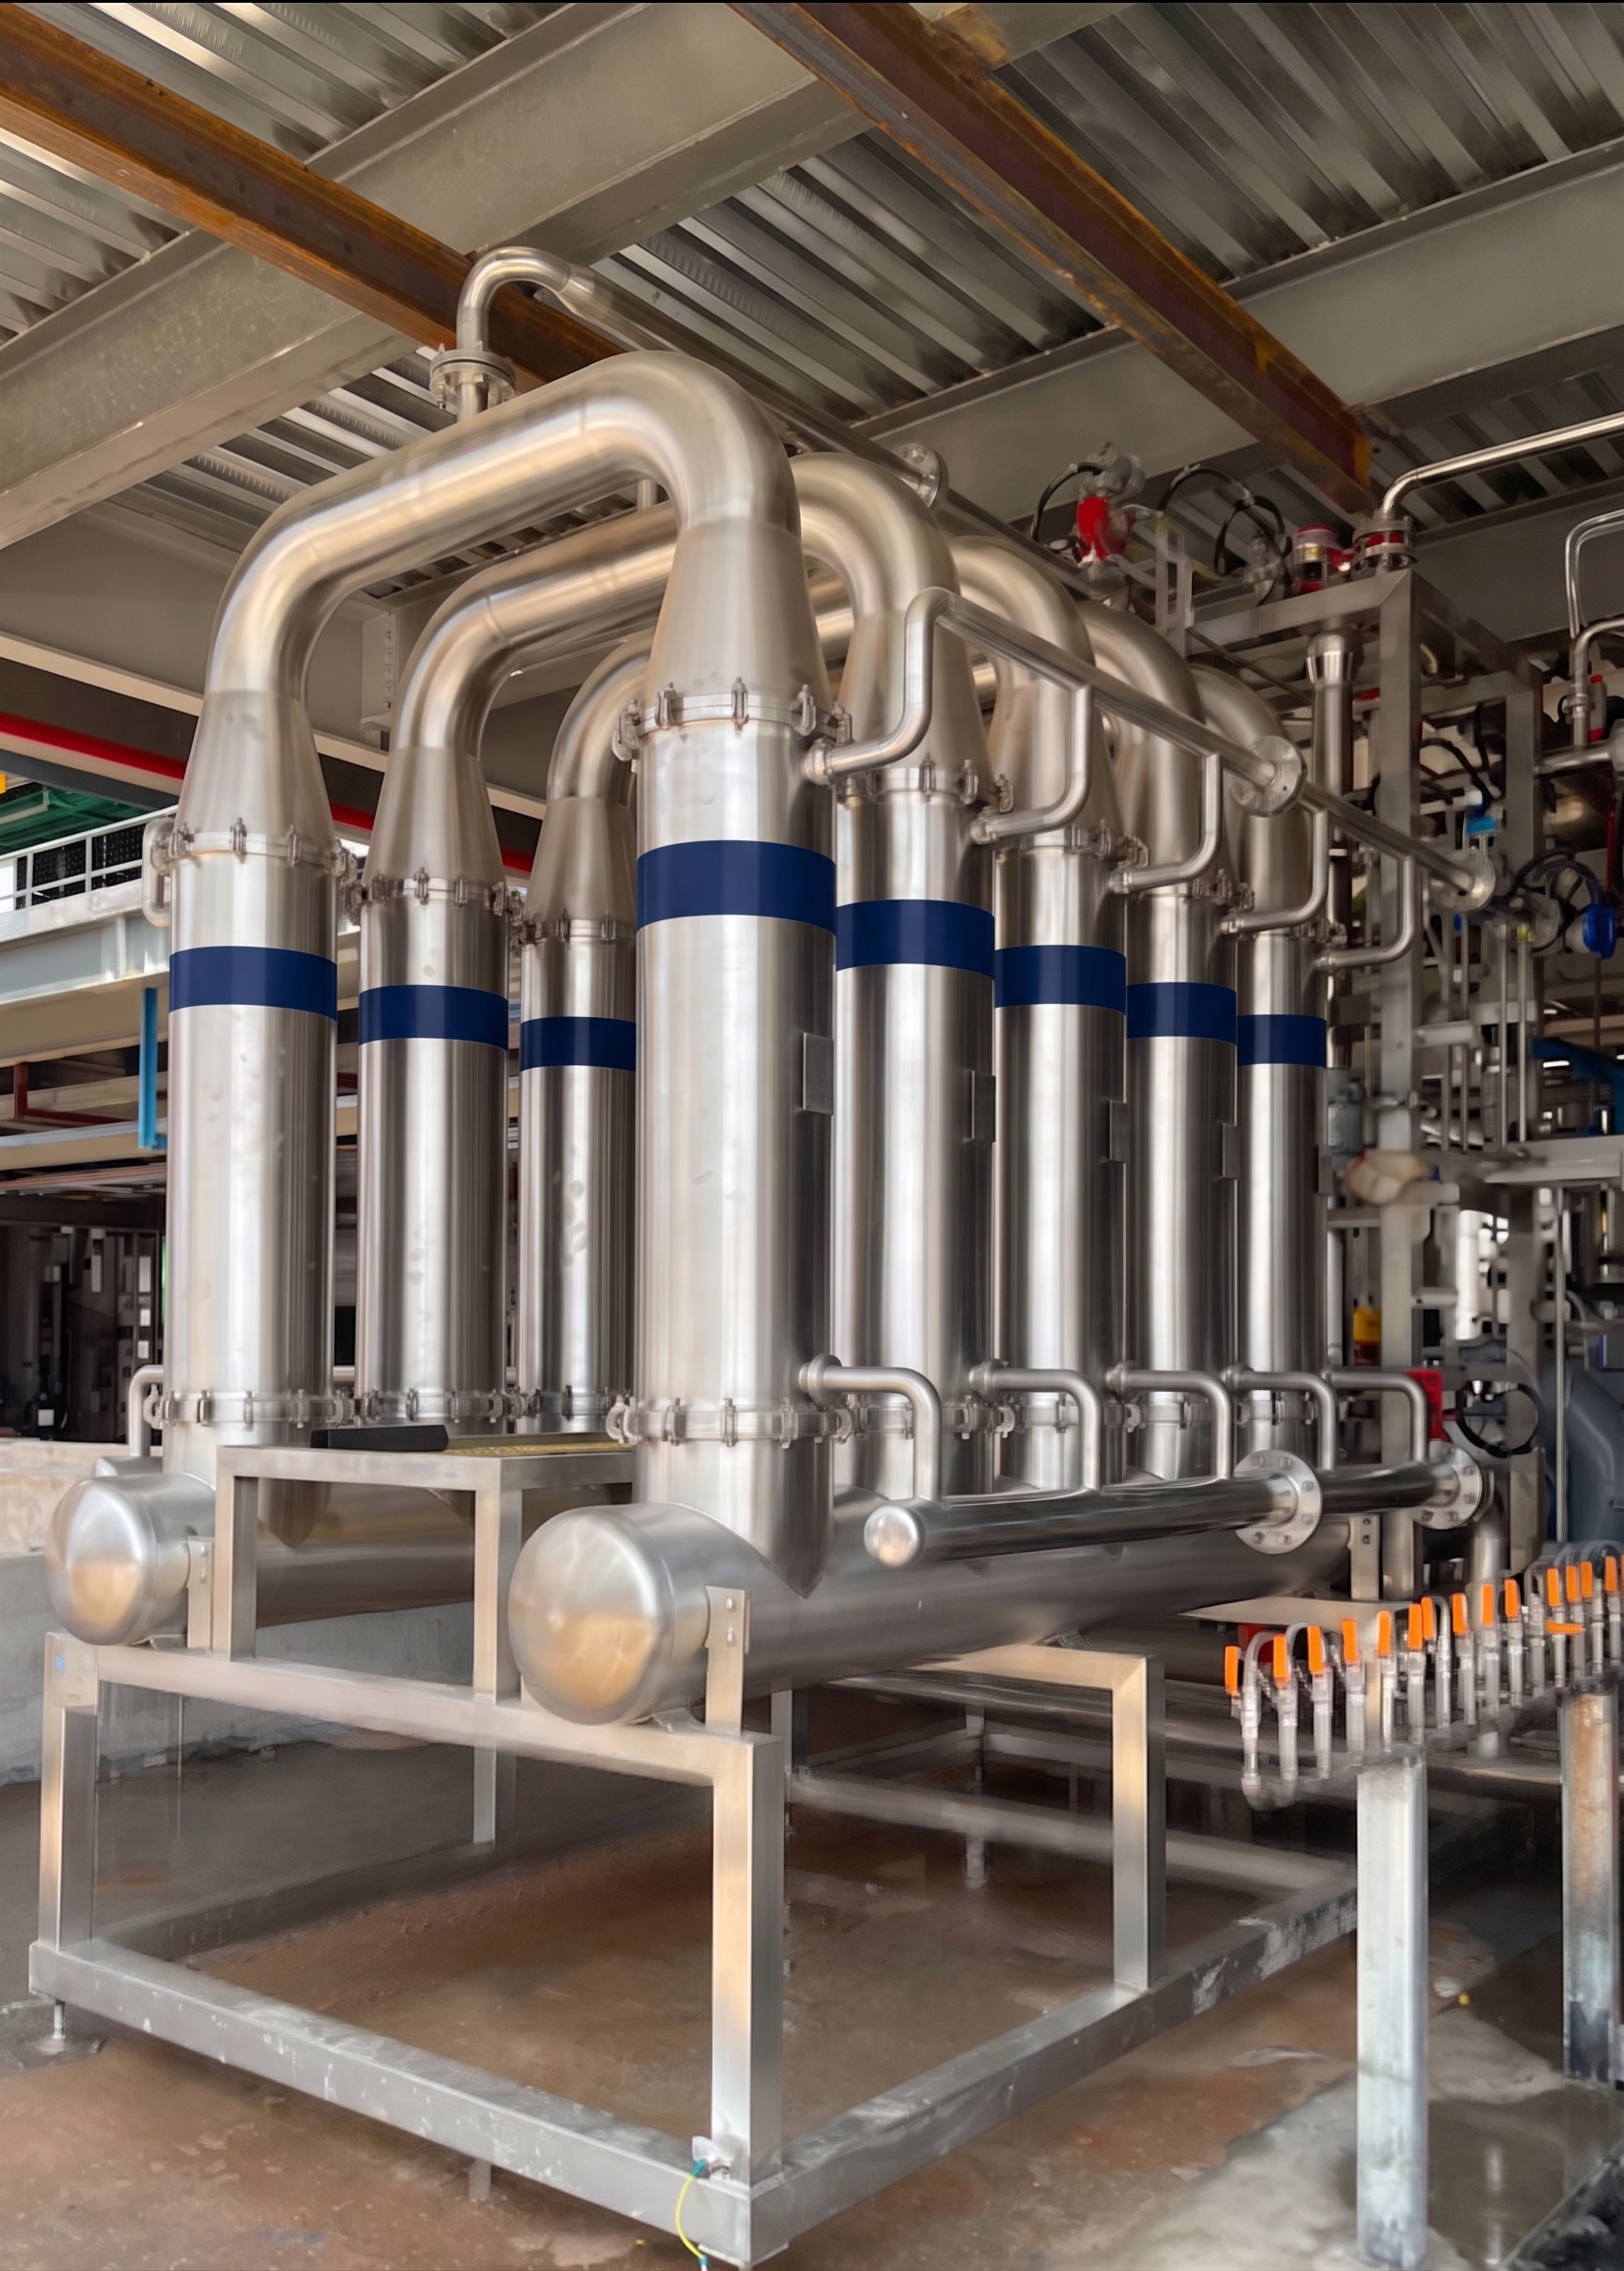
Ceramic ultrafiltration skids can be engineered with sanitary stainless steel piping and equipment, variable frequency drive (VFD) circulation pumps, flowmeters, pressure transmitters, and automated process valves.
Complete systems can be integrated with PLC/SCADA automation for monitoring and control of transmembrane pressure, flow rates, temperatures, filtration cycles, and cleaning sequences.
Our solutions are designed for reliable operation, efficient solids separation, controlled product recovery, and consistent filtration performance.
Applications
Ceramic membrane systems are suitable for enzymatic glucose and dextrose hydrolysate clarification, high-maltose and dextrin clarification, polyol process streams, fermentation broth clarification, organic acids, enzymes, amino acids, and other applications requiring efficient solid-liquid separation.
From process design to commissioning, each ceramic ultrafiltration solution can be tailored to feed characteristics, membrane requirements, production capacity, and downstream process conditions.